What Is Lead Loading in Historic Body Repair?
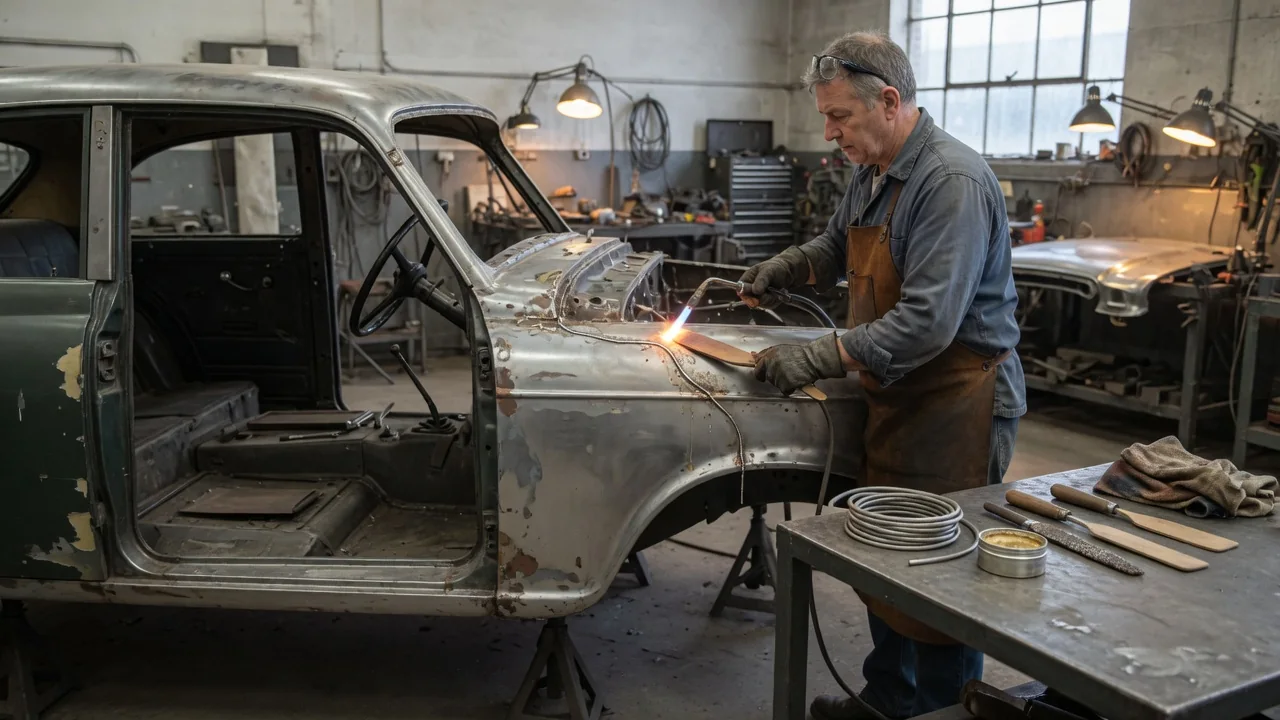
Lead loading, also called body soldering or leading, is the traditional way of filling seams, joints, and small surface irregularities on steel car bodies with a lead-tin alloy. Before polyester fillers became common, factories and coachbuilders used it to blend welded seams and smooth panel transitions. For anyone considering classic car lead loading today, it helps to understand what the material is, how it is applied, and what hazards it carries before deciding whether it belongs in a repair.
Traditional filler: what body lead actually is
Body lead is not pure lead. It is an alloy of lead and tin designed to soften gradually rather than melt all at once. Between fully solid and fully liquid, it passes through a pasty or plastic range, a temperature band in which the metal can be pushed and shaped like stiff clay. That property makes it workable on vertical and curved surfaces where ordinary solder would run off. Alloys with a higher proportion of lead generally have a wider working range, which is why body solders lean toward lead rather than toward the tin-rich solders used in plumbing or electronics.
Because the alloy bonds metallurgically to properly tinned steel, the filled area becomes part of the metal surface rather than a coating sitting on top of it. It does not absorb moisture, and it tolerates heat and some flexing of the surrounding panel. Historically, manufacturers used it on body seams, such as joins between roof panels and pillars, where a smooth, paintable transition was needed. Restorers still find original factory lead on many older steel-bodied cars, and recognizing it matters: it can be a period-correct part of the body rather than evidence of earlier damage repair.
Technique: tinning, applying, and shaping
Preparation decides whether the lead will stay put. The area must be taken down to clean, bright steel with no paint, rust, oil, or old filler, because solder will not wet contaminated metal. The steel is then tinned: a tinning compound, typically a flux paste containing powdered solder, is spread over the area and heated gently until it flows, then wiped with a clean rag while still hot. A properly tinned surface looks uniformly silvery. Dull or patchy spots indicate poor wetting, and lead applied over them is likely to lift later.
Next, a stick of body solder is warmed together with the tinned surface until its tip softens, and the softened metal is pressed onto the panel in small deposits. The worker then reheats those deposits just enough to bring them into the pasty range and spreads them with a hardwood paddle lubricated with tallow, beeswax, or a commercial paddle wax so the lead does not stick to the wood. The aim is to keep the metal plastic, never runny. Heat is applied in a broad, moving pattern with frequent pauses, because too much heat makes the lead slump and can distort thin sheet steel.
Once cooled, the lead is shaped with a body file, often a curved-tooth file, which cuts the soft metal cleanly without clogging as quickly as a fine-toothed file. The contour is checked by eye and by hand before primer. The final step is thorough cleaning: flux residue is often acidic and must be washed off and neutralized, or it can cause corrosion and paint adhesion problems under the finish.
Modern cautions: health, residue, and heat
Lead is toxic, and in body work the main exposure risk comes from dust rather than from brief heating. Filing produces coarse shavings, but sanding, especially with power tools, creates fine particles that are easily inhaled or carried home on clothing. Common precautions include filing instead of power sanding, wearing a properly fitted respirator rated for particulates, using disposable coveralls or dedicated work clothes, not eating or drinking in the work area, washing hands and face before breaks, and cleaning up with a HEPA-filtered vacuum or wet methods instead of sweeping. Children and pregnant people should be kept away from the area, and local rules may govern how lead waste is collected and disposed of.
Heat is the second concern. Leading requires a flame or other heat source close to paint, undercoating, seam sealer, interior trim, and fuel or brake lines, so the surroundings need to be cleared and a fire extinguisher kept within reach. Old paint stripped to prepare the area may itself contain lead, adding to the dust hazard. Flux chemicals can irritate skin and eyes, so gloves and eye protection belong in the routine.
Some suppliers offer lead-free body solders and tinning systems intended to reduce toxicity. Their handling and working range can differ from traditional body lead, so the manufacturer's instructions should be followed rather than assuming the old technique transfers unchanged.
Practical implications and limits
Leading is not a substitute for metal repair. It fills and finishes; it does not restore strength to rusted or torn steel, and laying it on thick over a poorly straightened panel adds weight and invites cracking. Sound practice is to bring the metal as close to final shape as possible with hammer, dolly, and welding, then use lead only for the last small amount of contour. The same principle applies to plastic filler, but the cost, weight, and effort of lead make overuse even less sensible.
The choice to use lead is often about originality and durability rather than necessity. Owners pursuing a correct restoration may want factory leaded seams reproduced in kind, while others accept a modern filler skimmed over sound metal. Lead's moisture resistance and bond to steel make it a reasonable choice at seams and edges that flex or see heat, but results depend heavily on preparation and skill. The process has a real learning curve, and practicing on scrap panels before touching a visible area is widely recommended. Original factory practices vary between body designs, so where lead was used on a particular car is best confirmed from its own documentation or marque-specific references.
When assessing an older body, keep in mind that a magnet will not stick to lead or to plastic filler, so a magnet alone shows only that non-steel material is present. Lead appears gray and metallic when lightly scraped, while plastic filler does not, which helps distinguish an original leaded seam from a later repair.